Food Condensed Milk Processing Plant
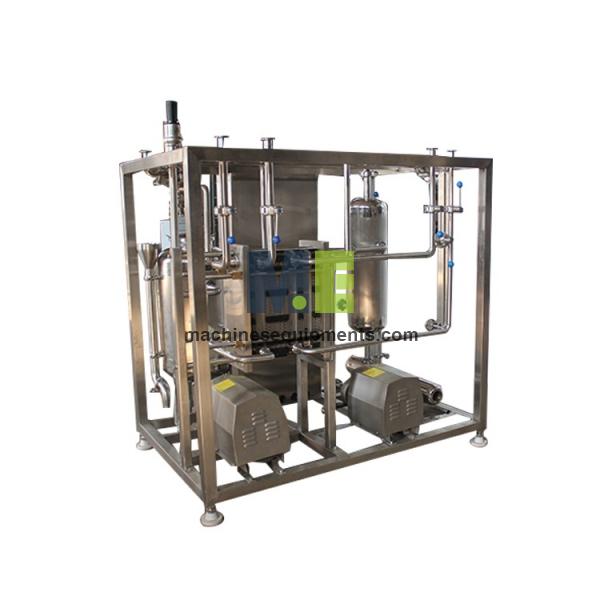
- Built to tender specification Capacities and configuration to your schedule
- FOB · CIF · CFR Quoted to your destination port
- Single units or bulk One machine or a full container
- Export documentation What customs at your end will ask for
Specification
1 value- Working capacity from
- 5 tons/d up to 100 tons/d
Standard model shown. Capacities, dimensions and configuration are built to tender specification on bulk orders. Warranty, installation service and operator training are agreed in the supply contract - send your requirement and we will quote against it.
About this unit
Sweetened condensed milk keeps without refrigeration for one reason: sugar concentration. The shelf life rests on osmotic pressure, and the process target is at least 62.5% sugar in the aqueous phase, which is the number the whole line is sized around. Fat and solids-non-fat are standardised before evaporation, and heat treatment does more here than kill organisms and enzymes; it stabilises the protein complex and governs how the product thickens in the can over months of storage. Get the heat treatment wrong and the viscosity drifts after shipment, which is a quality claim arriving long after payment. Sugar can be added as dry sugar or as syrup, and the two routes need different dosing and dissolving equipment. Tell us your daily milk intake and your can format.